Contents
In recent years, global events and technological innovation have reshaped the automotive industry's agenda. Inventory management, one of the industry's most critical disciplines, has been transformed as well. Traditional inventory management models are giving way to modern approaches, and static forecasts based on historical sales data and manual planning processes no longer do the job. With advances in AI-based analytics, machine learning and real-time data processing, automotive inventory management has become increasingly dynamic and predictive. This shift brings a number of strategic advantages: more accurate demand forecasts, optimized stock levels and proactive management of supply chain risks. Taken together, it shows the role technology now plays in inventory optimization across the automotive industry.
Why Inventory Management Matters in the Automotive Industry
Complex global production networks, a very wide range of parts and high sensitivity to demand fluctuations make the automotive industry one of the sectors where inventory management matters most. Building a car depends on tens of thousands of parts being in the right place at the right time. Global developments in recent years have made this even more pressing. Because automotive manufacturing involves so many different parts, multi-tier supplier networks and global production models, inventory management has become a critical operational discipline in the industry.
Since a car is built from thousands of components, the production process has become far more complex. Other factors make management harder still: the risk of production line stoppages, and the delicate cost balance between excess stock and stockouts. In recent years, crises such as the supply disruptions of the post-pandemic period have been added to the equation. So when we ask why inventory visibility and planning accuracy have become more important, the answer lies in the details of this whole picture.
Why Traditional Systems Fall Short in Inventory Optimization
Traditional inventory planning relies largely on statistical models built on historical sales data, fixed stock policies and manual planning processes. These approaches no longer meet today's needs. With its wide range of parts and its global, multi-tier structure, the automotive industry runs a highly data-intensive supply chain.
Traditional planning systems are mostly based on past sales trends and fail to capture complex shifts in demand behavior. Their demand forecasts therefore rest on static, limited data sets. In today's markets, however, demand is shaped by many variables, including economic indicators, regional market dynamics, promotions, model variants and even seasonal factors, so these systems struggle to anticipate sudden spikes or drops in demand.
In addition, production planning, procurement, logistics and sales data are often held in separate systems with little integration between them. Safety stock levels, reorder points and order quantities are usually set on the basis of fixed assumptions and stay unchanged for long periods. Updating these parameters manually for thousands of different parts is both time-consuming and error-prone, which is why traditional systems fall short. Unable to optimize multi-tier supply networks as a whole, they leave companies exposed to crises.
Efficiency Gains from AI-Driven Demand Forecasting
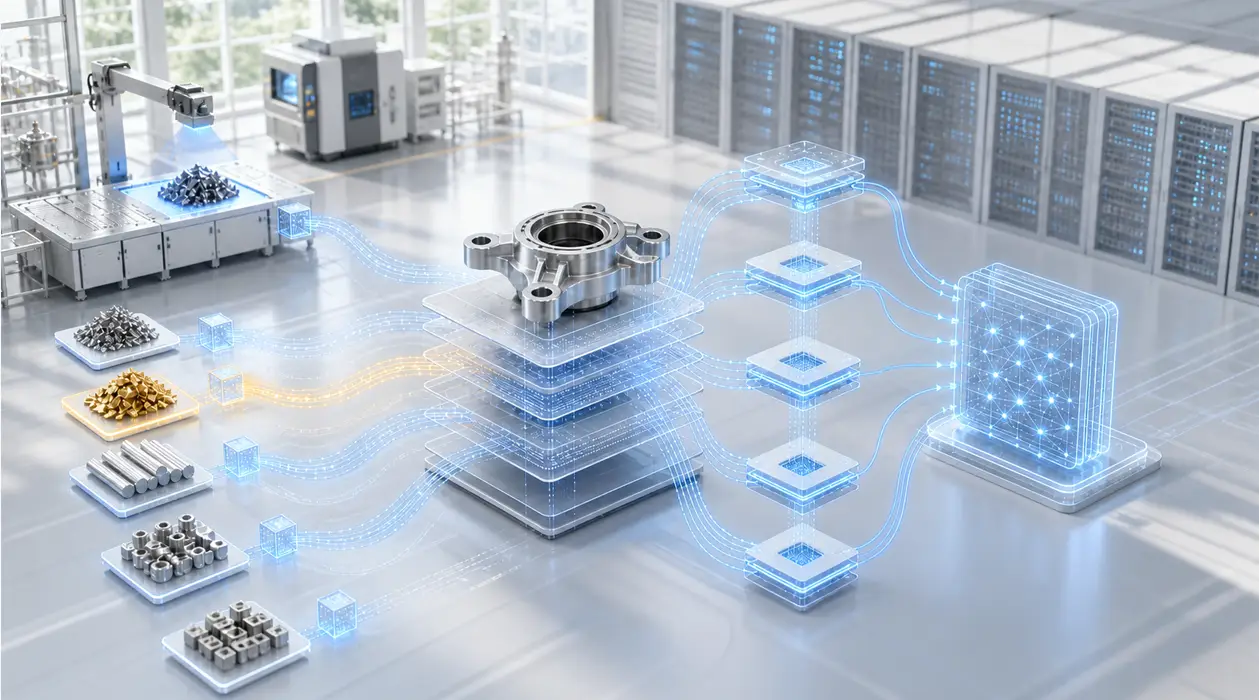
At the heart of AI-driven inventory optimization is the ability to handle data-intensive environments effectively, together with the deep analytical capability the technology provides. What does that mean in practice? Thousands of parts generate a massive flow of data between automotive manufacturers and their suppliers. Faced with mountains of data such as extensive sales histories, production plans, parts consumption rates, supplier lead times, economic indicators and even weather, traditional systems are simply overwhelmed.
This is where machine learning models come in, as they can process and analyze all of this data at once. They differ from traditional statistical forecasting methods because they can detect complex relationships and hidden patterns and help prevent potential crises. They deliver highly precise forecasts because they can significantly improve demand forecast accuracy. This makes it possible to avoid both overstocking and shortages. It frees companies from a heavy cost burden and benefits both supplier relationships and, ultimately, brand reputation. That can make a decisive difference in the industry.
Unlike traditional models, AI-driven demand forecasting systems can analyze much larger data sets. Sales history, market trends, economic indicators, customer behavior and supply chain data are all assessed within the same model. Machine learning algorithms analyze the complex relationships within this data and produce more accurate demand forecasts. As a result, both excess stock and stockouts can be reduced significantly. Research suggests that AI-based forecasting systems can improve demand forecast accuracy by around 20%. Given that figure, it is clear that the efficiency gained from better forecast accuracy alone is a major advantage for companies.
Data Analytics and Continuously Learning Systems
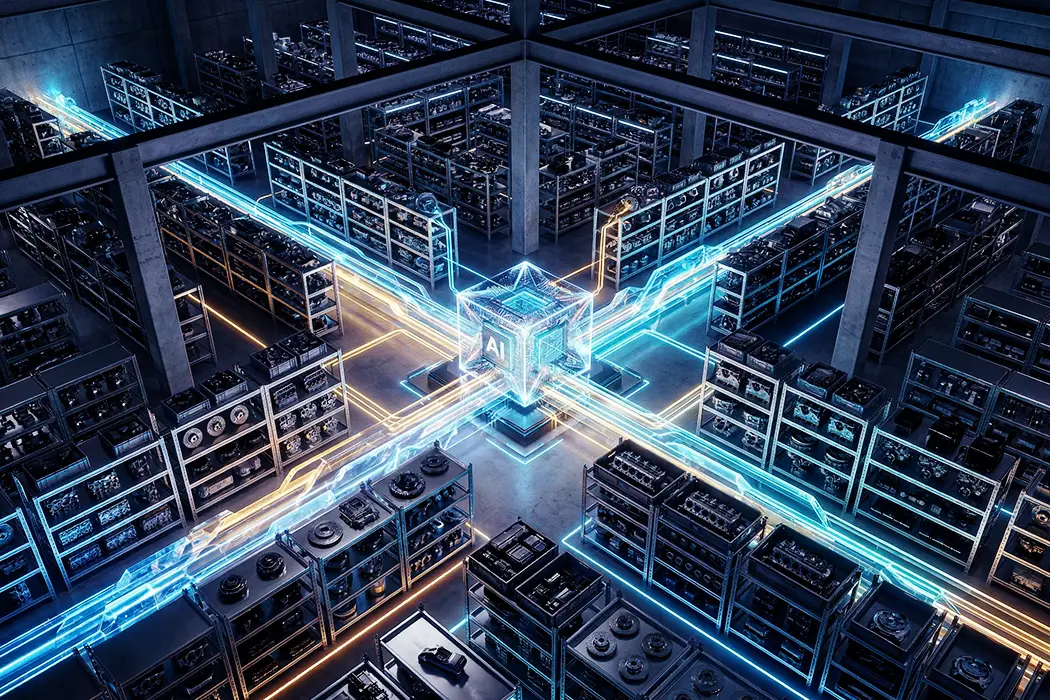
AI-driven optimization systems can analyze the multi-tier structure of the supply chain as a whole and determine how much of each part should be stocked at each location. This means that regional differences in demand, supplier lead times and logistics costs can all be evaluated within a single model. With the help of AI, automotive companies are reported to have cut inventory levels by around 20% while maintaining service levels. In other words, AI gives inventory optimization real strength in managing multi-tier supply chains. Because vehicle manufacturers typically work with hundreds or even thousands of suppliers, and stock has to be held at every tier of that network, this capability strengthens their competitive advantage.
Next-generation systems take a more dynamic approach based on data analytics, AI and real-time data integration. Their key difference is that they turn inventory planning from a static forecasting exercise based solely on historical data into an optimization process that keeps learning and updating itself. In current applications, AI does more than forecast; it works as a continuously learning optimization engine. It refines its algorithm-based decisions over time and keeps learning as it goes. If demand for a part rises faster than expected, for example, the system can automatically recalculate stock policies and adjust order quantities. That makes a huge difference. Learning-based models of this kind have been found to reduce costs more than traditional models and to deliver more resilient results, especially during supply chain disruptions. This highlights their strategic value for crisis management and communication.
Real-Time Data and Operational Flexibility in Inventory Management
In the automotive industry, AI-driven inventory optimization is used not only in planning but also actively in day-to-day operations. Sensors, digital twins, IoT (Internet of Things) devices and warehouse automation systems allow stock movements to be tracked in real time. This data feeds into AI models, so the system can detect anomalies or potential risks in stock levels at an early stage. If a particular part is being consumed on the production line faster than expected, for example, the system can automatically update procurement or production plans. This turns inventory management from a static planning activity into a real-time decision-making mechanism.
AI also treats automotive inventory management as part of wider supply chain optimization. Modern systems bring demand forecasting, network optimization, lead time prediction and exception management together on a single platform. This removes data gaps between planning, logistics and production, and the system becomes self-optimizing, driven by continuously updated real-time data. Automotive companies gain an edge from more flexible, data-driven inventory management models, especially in crisis-prone situations such as geopolitical risks and post-pandemic supply disruptions.
Conclusion
Today, in complex, data-intensive and multi-tier industries such as automotive, virtually every technological advance takes on a strategic role. Inventory management has long been a front-line operational function in this industry, focused mainly on cost control, and it is now being reshaped along these strategic lines.
Frequently Asked Questions (FAQ)
Why is inventory management critical in the automotive industry?
Complex global production networks, a very wide range of parts and high sensitivity to demand fluctuations make inventory management operationally critical in the automotive industry.
Why do traditional systems fall short in inventory optimization?
Traditional planning systems rely on historical sales data and static forecasting methods, so they struggle to anticipate sudden shifts in demand in today's markets.
How much efficiency do AI-driven forecasting systems deliver?
Research suggests that AI-based forecasting systems can improve demand forecast accuracy by around 20%.
How do continuously learning systems contribute to inventory optimization?
If demand rises faster than expected, the system can automatically recalculate stock policies and adjust order quantities using learning-based algorithms.